PRODUCT
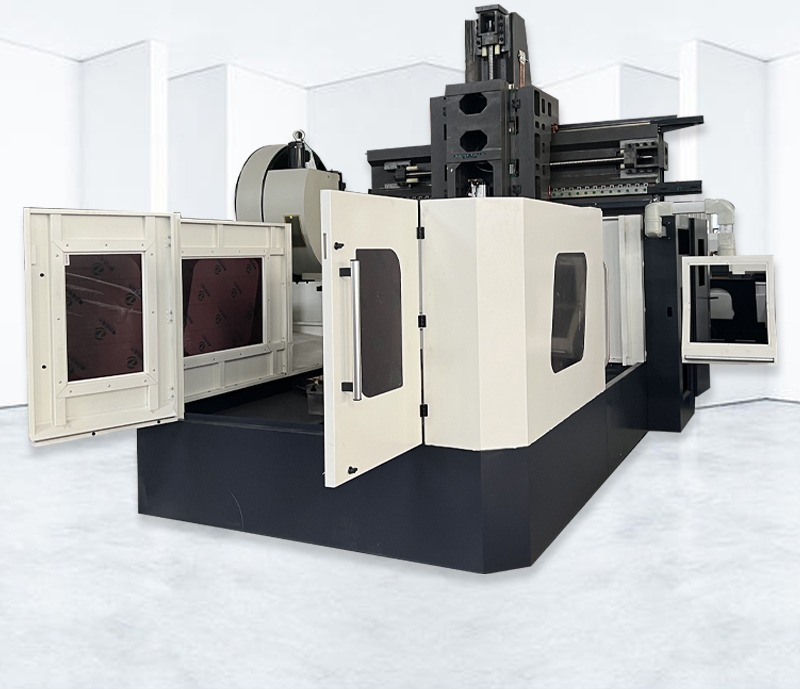
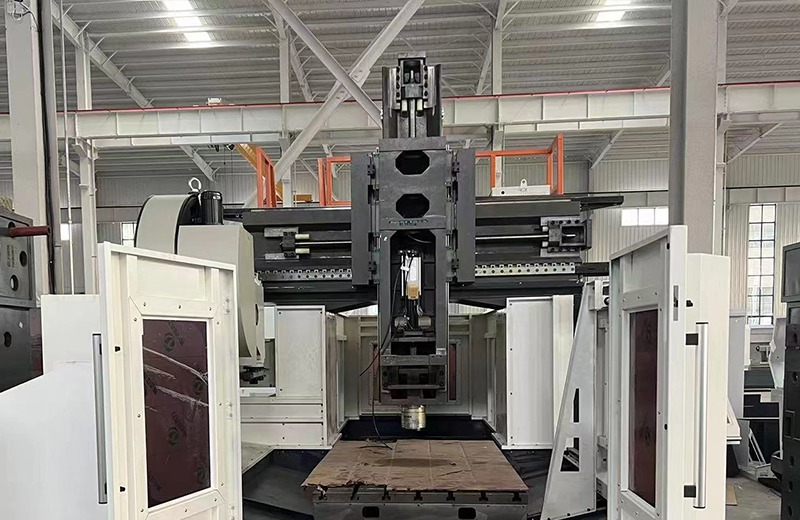
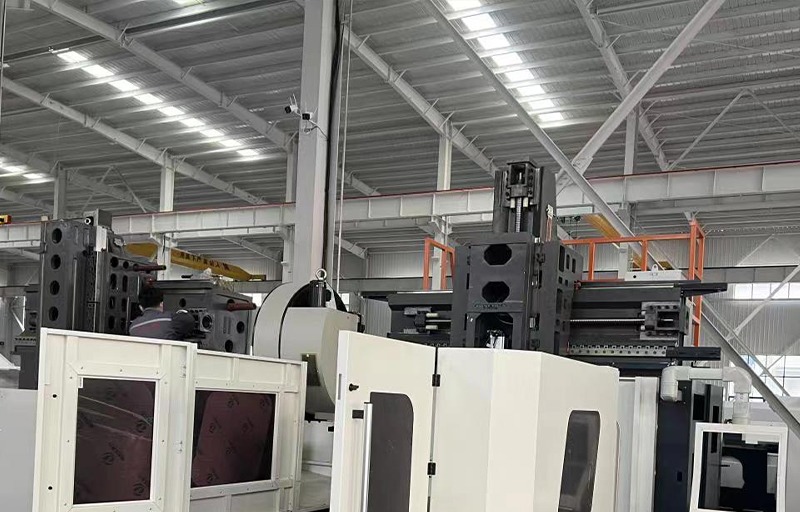
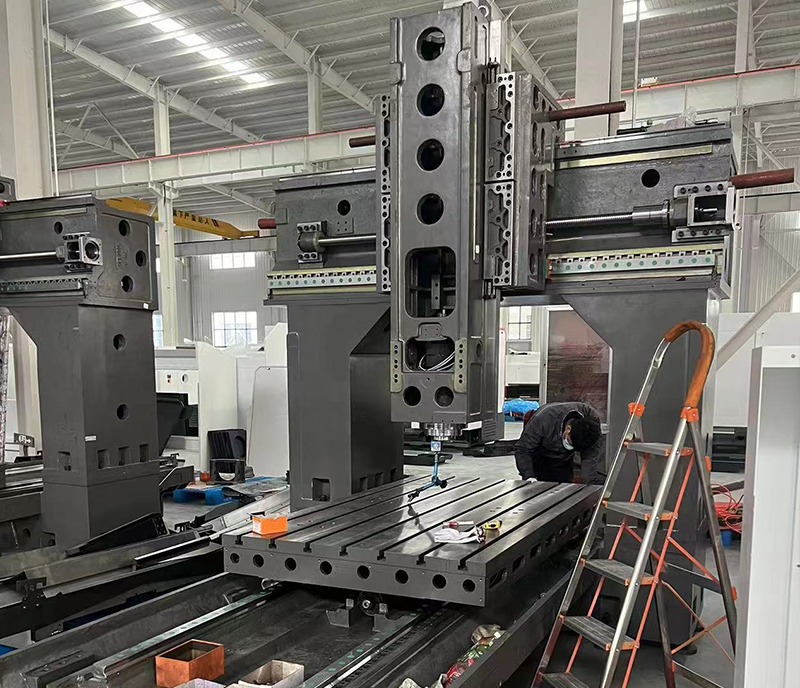
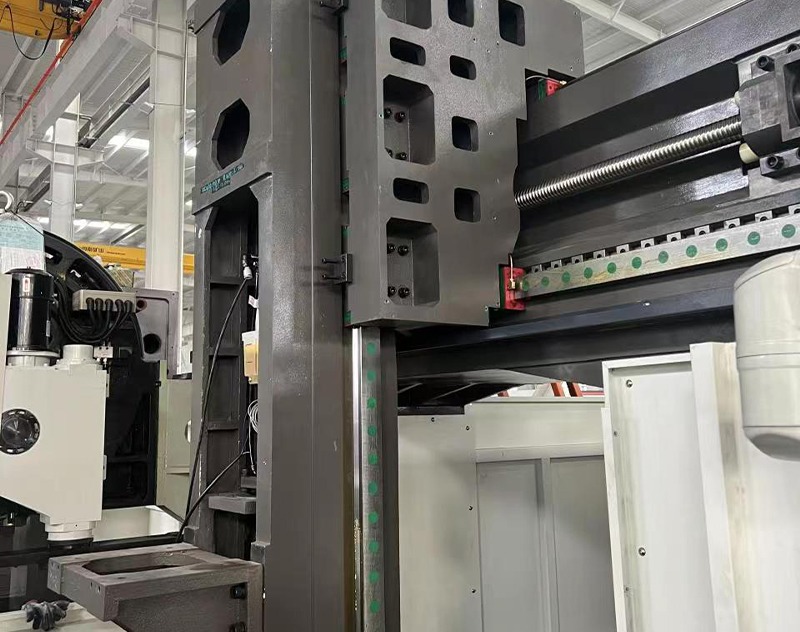
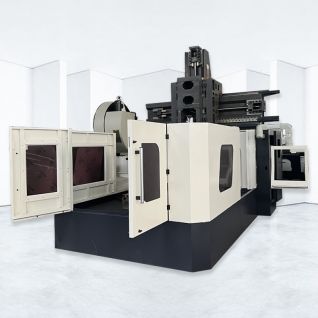
GMC1813 CNC Gantry Milling Machine
The GMC1813 is a double column CNC gantry milling machine with a 2000 × 1000 mm table rated for 4000 kg, travels of 1800 mm in X, 1300 mm in Y and 770 mm in Z, and a 1300 mm gantry width. It is built for large plates, dies, machine bases and weldments that do not fit a vertical machining centre. Overseas after-sales service and CE certified.
GMC1813 CNC Gantry Milling Machine
The GMC1813 is a double column CNC gantry milling machine for workpieces that a vertical machining centre cannot take: large plates, press and injection moulds, machine tool bases, frames, weldments and long structural parts. The table is 2000 × 1000 mm and rated for 4000 kg, travel is 1800 mm in X, 1300 mm in Y and 770 mm in Z, and the machine weighs 16 tonnes. Because the spindle is carried on a cross rail between two columns instead of on a single vertical column, the cutting force is taken symmetrically and the spindle can reach the full table area without the overhang that makes a C-frame machine lose rigidity at the edge of a big part. Milling, drilling, tapping and boring are carried out in one clamping, which is what keeps hole positions and face parallelism tied to a single datum.
Key Features
- Working table 2000 × 1000 mm, load capacity 4000 kg
- X axis travel 1800 mm, Y axis travel 1300 mm, Z axis travel 770 mm
- T-slots 7 × 150 × 22 mm for clamps, angle plates and fixtures
- Spindle end face to table distance 150 - 920 mm
- Gantry width 1300 mm, double column structure with a rigid cross rail
- Machine dimensions 5300 × 3500 × 3800 mm, machine weight 16 T
- Ground guideways on all axes for positioning stability under heavy cuts
- Suited to large plates, moulds, machine bases and welded frames
- Spindle, control and tooling configuration quoted against the actual part
Double Column Structure and Why It Holds Accuracy
A gantry machine puts the spindle on a cross rail that is supported at both ends by two columns. When the cutter works at the edge of a 2000 mm plate, the load path runs down through the rail into both columns and into the bed, so the deflection at the tool tip stays small and stays symmetrical. On a single column machine of comparable table size, the same cut at the far edge of the table has a long unsupported overhang behind it, the head drops and twists, and the flatness of the machined face changes from one side of the part to the other. That difference shows up directly in the parts that matter here: a die with a shut-off face that must close, a machine base with mounting pads that must be coplanar, a frame where two bores must stay parallel over two metres. It is also why gantry machines are the standard for large work rather than an oversized version of a vertical machining centre.
What the 2000 × 1000 mm Table and 1800 mm Travel Mean
The table is 2000 mm long, but X axis travel is 1800 mm. Those two numbers are not the same, and the difference matters when a job is quoted. A part up to about 1800 mm long can be machined over its full length in one set-up. A part longer than 1800 mm will need a second clamping position, with the datum re-established and the joint between the two set-ups blended; on a long part this is normal practice, but it has to be planned and it has to be priced. The same logic applies across the table: the Y travel of 1300 mm covers the 1000 mm table width with margin for positioning the cutter beyond the workpiece edge. If your part is longer than 1800 mm, tell us at the quotation stage and we will confirm the set-up sequence instead of leaving you to discover it after the machine is on the floor.
Height, Gantry Width and the Real Workpiece Envelope
Three dimensions decide whether a part fits: table, height and width. The table is 2000 × 1000 mm. The spindle end face can sit between 150 mm and 920 mm above the table, and Z axis travel is 770 mm, so the practical height of a part that can be machined is set by the 770 mm of Z stroke together with the length of the tool in the spindle, not by the 920 mm maximum clearance, which is only the loading position. The gantry width is 1300 mm, but the table is 1000 mm wide: the 1300 mm is the clear distance between the columns, so the real limit on workpiece width is the 1000 mm table plus whatever the fixture adds. We state these three numbers separately because a customer who plans against the larger figure of each pair will order a machine that cannot reach his part, and we would rather settle the envelope on the drawing than on the shop floor.
Milling, Drilling, Tapping and Boring in One Set-Up
The value of a gantry machine on large work is not only size, it is that the operations stay on one datum. With the part clamped once on the 2000 × 1000 mm table and located in the 22 mm T-slots, the machine face mills the top, drills and taps the mounting holes, mills the pockets and bores the bearing seats without the part being released and re-indicated. Every re-clamping of a part weighing up to 4000 kg introduces a new error: the part settles on the fixture, the datum shifts, and the hole pattern no longer lines up with the face that was machined before. Doing the work in one set-up removes that error at the source. For deep pockets and long boring bars, the 150 mm minimum spindle-to-table distance allows the head to come down close to the work, which keeps the tool short and the cut rigid.
Applications and Materials
The GMC1813 is used in mould and die shops, machine tool building, general machinery, automotive tooling, energy equipment, railway and heavy fabrication. Typical parts are press and injection mould bases, die plates, machine beds and columns, welded frames, bearing housings, large flanges and structural components with machined faces and hole patterns. It machines carbon steel, alloy steel, stainless steel, cast iron, aluminium and copper alloys, with cutting data set by the material, hardness, fixture rigidity and finish requirement. Where a part is too large or too heavy for a vertical machining centre, this is the class of machine that keeps the work in-house instead of sending it out for subcontract milling.
Technical Specifications
| Model | GMC1813 |
| Working table size | 2000 × 1000 mm |
| Table load capacity | 4000 kg |
| T-slot (number × pitch × width) | 7 × 150 × 22 mm |
| X axis travel | 1800 mm |
| Y axis travel | 1300 mm |
| Z axis travel | 770 mm |
| Spindle end face to table distance | 150 - 920 mm |
| Gantry width | 1300 mm |
| Machine dimensions (L × W × H) | 5300 × 3500 × 3800 mm |
| Machine weight | 16 T |
Delivery, Installation and Service
The machine is shipped as a complete unit at 5300 × 3500 × 3800 mm and 16 T, so lifting capacity, floor loading, door width and the route into the workshop should be checked before delivery. Installation is supported with foundation and levelling guidance, commissioning checks and operator training on the control and on work-holding for large plates. Spare parts and technical support are handled by our overseas after-sales service, and the machines are CE certified. Spindle speed range, spindle power, taper, tooling and control configuration are specified against the actual workpiece and cutting process, and are confirmed in the quotation rather than assumed from a generic list.
Request a Quote
Send us the part drawing, the material, the batch size and the operations you need, and we will confirm the GMC1813 configuration, the work-holding arrangement, the price, the delivery time and the technical support. We provide overseas after-sales service and CE certified machines.