PRODUCT
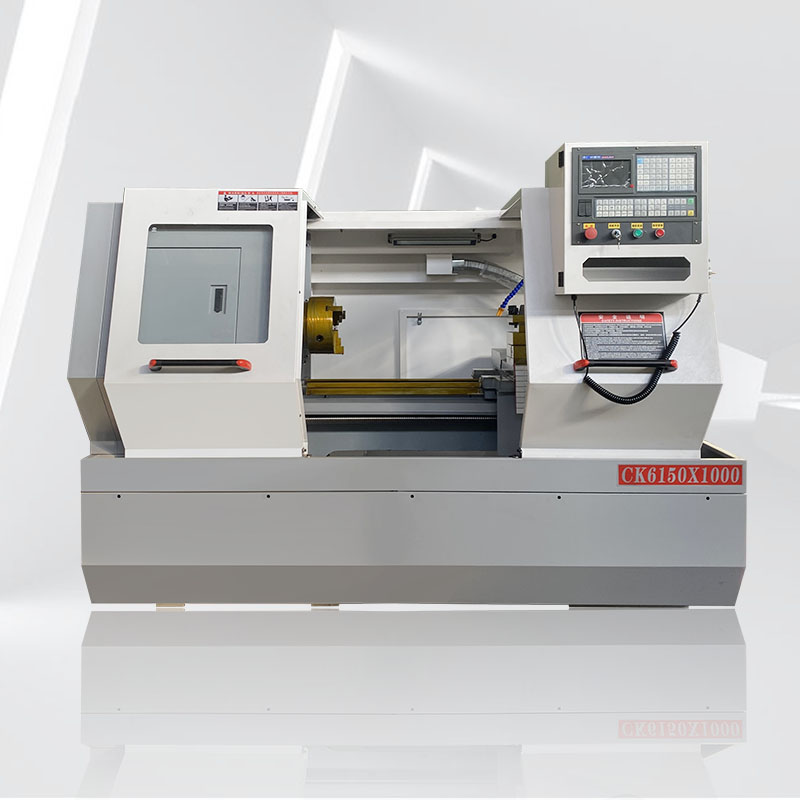
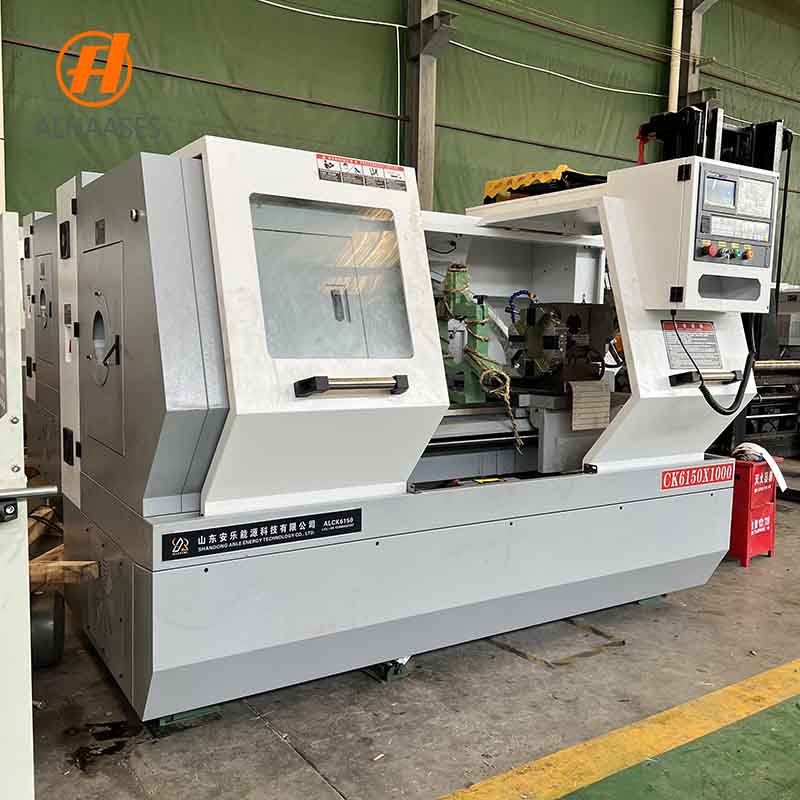
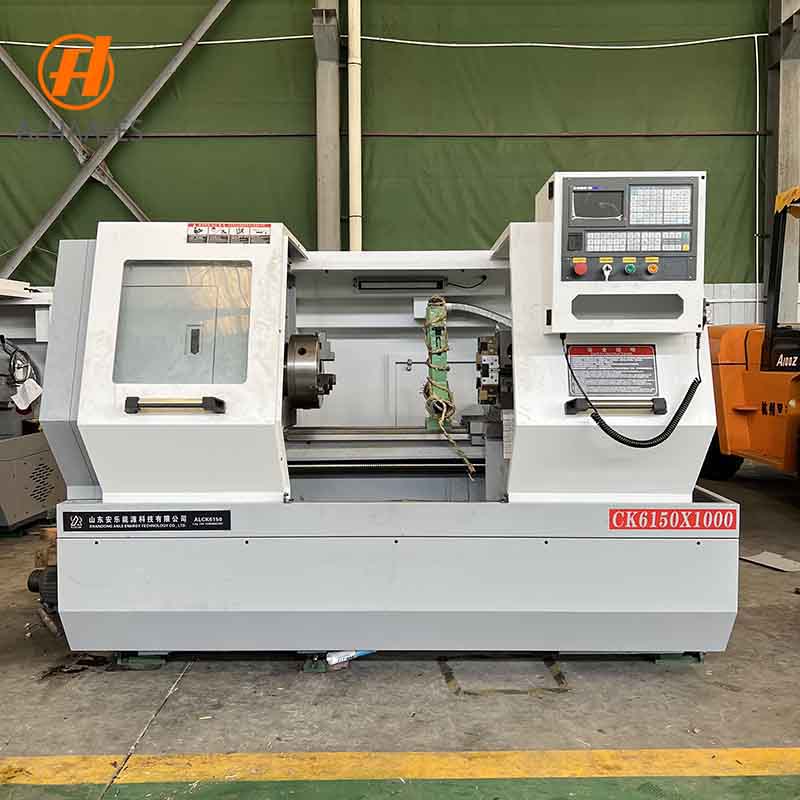
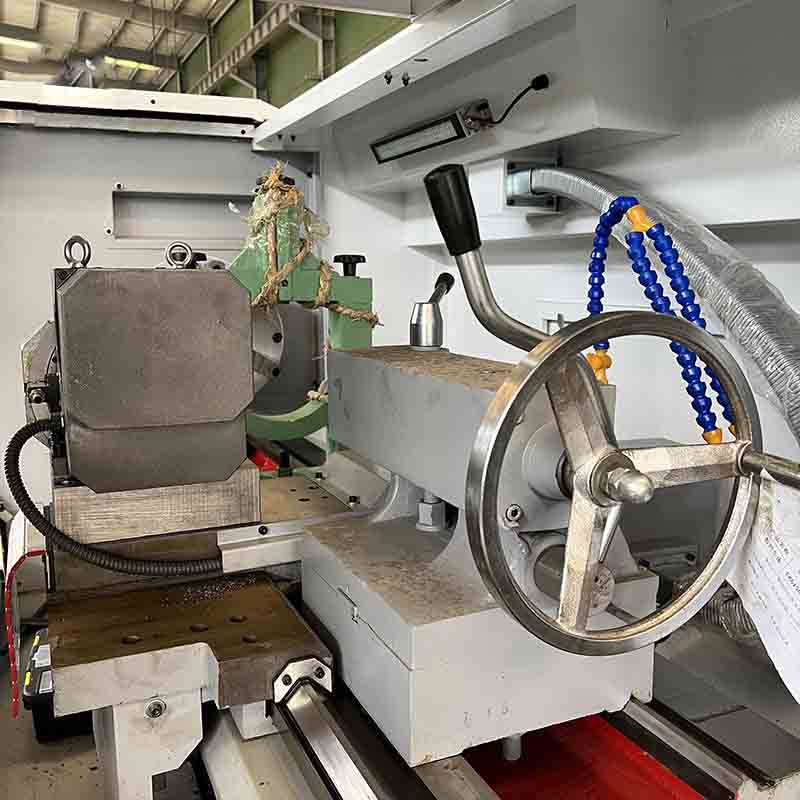
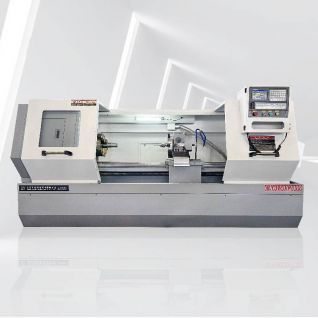
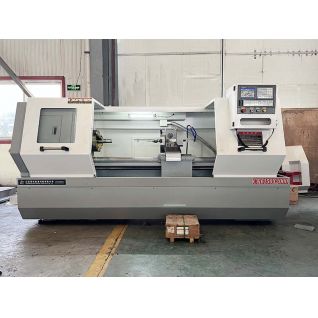
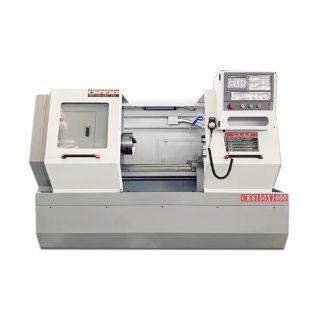
ALCK6150X1000 Flat Bed CNC Lathe
The ALCK6150X1000 is a flat bed CNC lathe for shaft and disc work up to 1000 mm: Φ500 mm swing over the bed, Φ290 mm over the slide, Φ82 mm spindle bore, X/Z strokes of 300 and 1000 mm with 0.001 mm minimum displacement. CE certified, with installation and overseas after-sales support.
ALCK6150X1000 Flat Bed CNC Lathe
The ALCK6150X1000 is the 1000 mm machine on our flat bed CNC lathe platform: Φ500 mm swing over the bed, Φ290 mm over the slide, a Φ82 mm spindle bore and X/Z strokes of 300 and 1000 mm. It is built for shops that turn shafts, tubes and medium-sized disc parts in daily production and need a machine that holds size without being babysat.
Flat bed, hardened and ground guideways, a bed that is one casting rather than bolted sections — that combination is why this class of lathe still outlasts lighter slant bed machines on heavy interrupted cuts. The machine is CE certified and backed by our overseas after-sales network.
Key Features
- Φ290 mm swing over the slide — the working diameter with the tool mounted. This is the figure to plan the process around.
- Φ500 mm swing over the bed — clearance for irregular castings and faceplate work, not a turning capacity.
- 1000 mm maximum processing length — shaft work between centres with the tailstock in place.
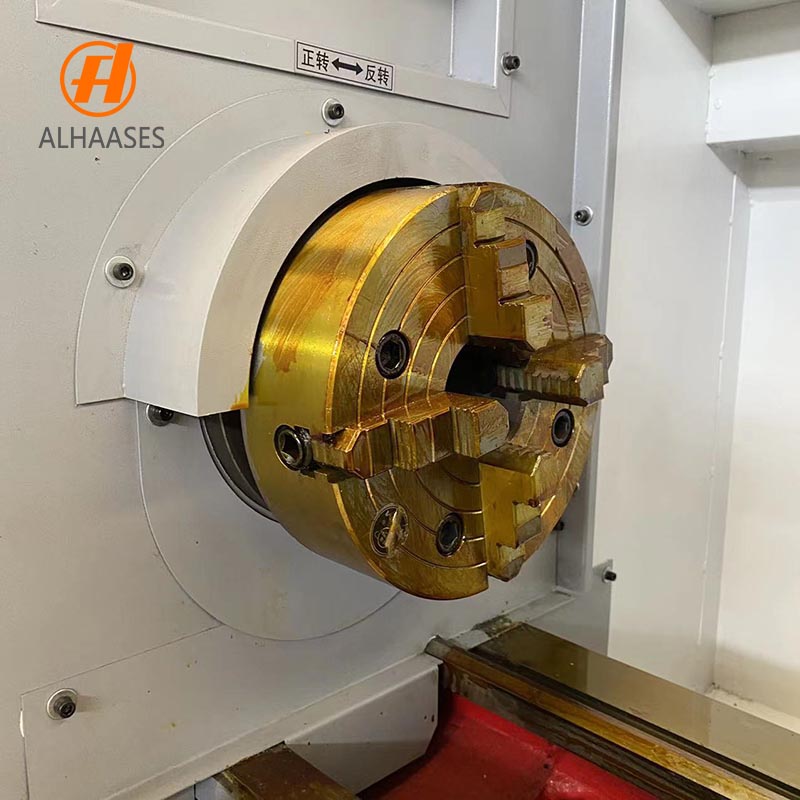
- Φ82 mm spindle bore — bar and tube work through the spindle instead of hanging out of the chuck.
- X/Z stroke 300 / 1000 mm — 300 mm of cross travel is enough for a full range of tooling on a Φ500 class bed.
- 0.001 mm minimum displacement — the control resolution on both axes, so tool offsets and wear compensation can be dialled in fine.
- 3030 × 1600 × 2050 mm footprint — a machine that fits a normal bay without a special foundation.
Φ500 Over the Bed, Φ290 Over the Slide
Two swing figures appear on every flat bed lathe, and quoting only the larger one is how a machine gets bought for work it cannot do.
The Φ500 mm over the bed is a clearance figure: the largest diameter that will physically rotate above the bed with nothing in the way. The Φ290 mm over the slide is the working figure: with the toolpost mounted and a tool in it, this is the diameter you can actually turn along its length.
The difference is 210 mm in diameter — 105 mm of radius that the cross slide, toolpost and tool occupy. That 105 mm is real estate you do not get to cut in.
The table also lists a maximum cutting diameter of Φ500 mm. Read it correctly: that figure applies to face work and to short parts machined in the gap, where the tool reaches across the part face rather than travelling along its length. For turning a cylinder — the normal case — plan against Φ290 mm. If your part needs more than Φ290 mm turned diameter, send the drawing before you order; a larger model in the same range is the honest answer, and we will say so rather than let the machine arrive undersized.
Φ82 mm Spindle Bore for Bar and Tube Work
An Φ82 mm bore is the difference between feeding bar through the spindle and hanging it out of the chuck. Bar fed through the bore is supported close to the cut, the remnant is short, and the cycle repeats without re-chucking — which is what makes bar work profitable on a lathe of this size.
Leave a working clearance when specifying bar stock: a bore is a nominal diameter, and a bar that is a tight fit will mark the bore and fight you on every load. Tell us the stock diameter and length you run, and we will confirm the chuck, the bar feed interface and the remnant length that goes with it.
1000 mm Between Centres, Φ65 mm Tailstock Sleeve
With the tailstock in place the machine takes shaft work up to 1000 mm of machining length, supported at the free end by a Φ65 mm sleeve. That is the difference between turning a long shaft that stays straight and turning one that springs away from the tool.
For shafts at the top of the length range, a steady rest is normally specified as well, because a tailstock supports the end but not the middle. If your parts are long and slender, say so at quotation stage — the support arrangement is decided before the machine is built, not after it lands.
0.001 mm Resolution, and What It Does Not Mean
The control commands both axes in 0.001 mm steps. That is the resolution of the system, not a promise about accuracy. Positioning accuracy and repeatability come from the ballscrews, the guideways, the thrust bearing arrangement and the thermal behaviour of the bed — and on a lathe, from how the part is held.
What the fine resolution is good for in daily work: tool wear compensation can be applied in small increments instead of jumping 0.01 mm at a time, and offsets after a tool change can be dialled in without overshooting. On finishing passes that is the difference between holding a tolerance band and living at one edge of it.
We quote accuracy figures separately, measured on the machine before shipment. Ask for them if the tolerance on your drawing is the deciding factor.
Applications and Typical Parts
The ALCK6150X1000 is used where shafts, tubes and disc parts are turned in quantity:
- Shafts and axles — stepped shafts, splined shafts, pump shafts, motor shafts
- Tubes and hollow parts — bushings, sleeves, hydraulic cylinders, pipe adaptors
- Flanges and discs — flanges, end caps, spacers, pulleys, gear blanks
- General engineering — threaded parts, pins, rollers, repair work and job shop batches
It machines carbon steel, alloy steel, stainless steel, cast iron, brass and aluminium with the appropriate inserts and parameters. For castings and forgings with interrupted cuts, tell us the blank condition so the configuration and tooling are matched to it.
CNC System and Configuration Options
The machine is supplied with a production CNC system and configured against your process. Options typically specified with this model include:
- Chuck type and size — three-jaw, independent four-jaw or collet chuck for bar work
- Toolpost arrangement — four-station automatic or quick-change manual, depending on batch size
- Tailstock and steady rest for shaft work at the top of the length range
- Chip conveyor and coolant system matched to the material being cut
- Bar feed interface matched to your stock diameter and length
- Tool setter and workpiece counter for unattended cycles
Configuration drives both cycle time and price. Final specification is confirmed against your drawing and monthly quantity before quoting, so the machine that arrives matches the process you described.
Installation, Commissioning and Support
The machine ships as a complete unit and needs a level floor and a normal industrial power supply, not a special foundation. We supply the foundation drawing, electrical schematic and parameter list before the machine leaves the factory, so site preparation can start while it is in transit.
Commissioning covers levelling, spindle runout check, axis alignment, tool setting and a first-part run against your drawing. Training for operators and maintenance staff is included. Our overseas after-sales service network keeps spare parts and technical support available for the working life of the machine, and responds in English, Spanish, Russian or Arabic.
Technical Specifications
| Item | Unit | ALCK6150X1000 |
| Max. swing dia. over bed | mm | Φ500 |
| Max. swing dia. over slide | mm | Φ290 |
| Max. cutting diameter | mm | Φ500 |
| Max. processing length | mm | 1000 |
| X / Z axis max. stroke | mm | 300 / 1000 |
| X / Z axis min. displacement unit | mm | 0.001 |
| Spindle hole diameter | mm | Φ82 |
| Tailstock sleeve diameter | mm | Φ65 |
| Machine dimensions | mm | 3030 × 1600 × 2050 |
The table is the platform specification. Weight and the exact configuration are confirmed on the quotation — we do not quote a weight we have not confirmed for the build. And once more: Φ500 mm is swing over the bed (clearance), Φ290 mm is swing over the slide (working limit). Plan against Φ290 mm.
Why Choose ALCK6150X1000
- CE certified — documentation supplied for EU import and site acceptance.
- Overseas after-sales service — engineers and spare parts support in Europe, with response in four languages.
- Φ290 mm working diameter on a 1000 mm bed — shaft and disc work on one machine.
- Φ82 mm spindle bore — real bar capacity, not a bar that hangs out of the chuck.
- 0.001 mm resolution — fine wear compensation and clean tool offsets.
- Flat bed with hardened, ground guideways — holds up under interrupted cuts and heavy stock removal.
Send us a drawing, the blank condition and the monthly quantity. We will confirm the configuration, quote it, and tell you plainly if another model fits better.