PRODUCT
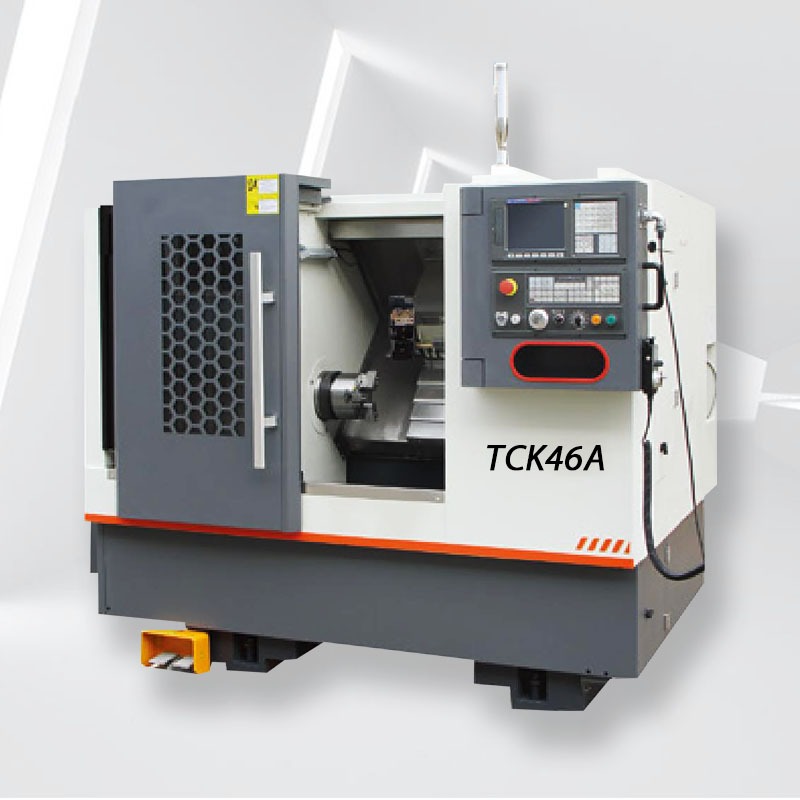
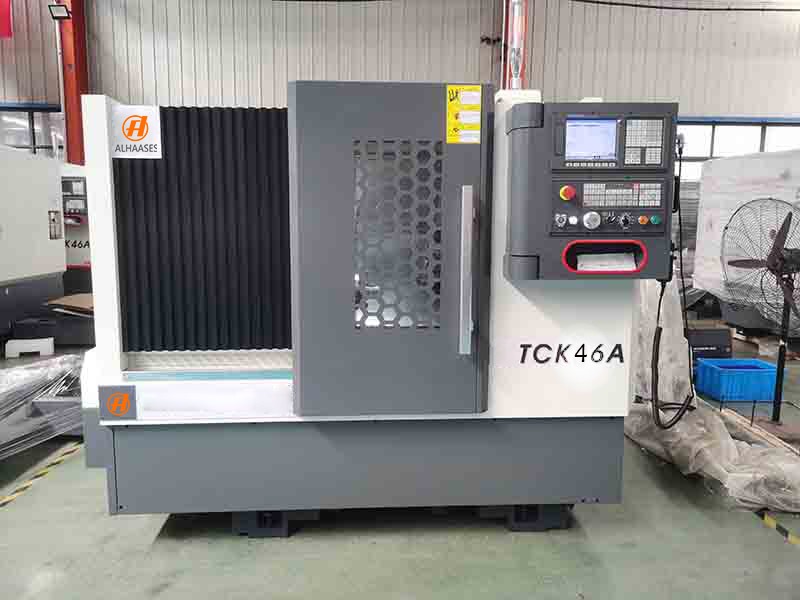
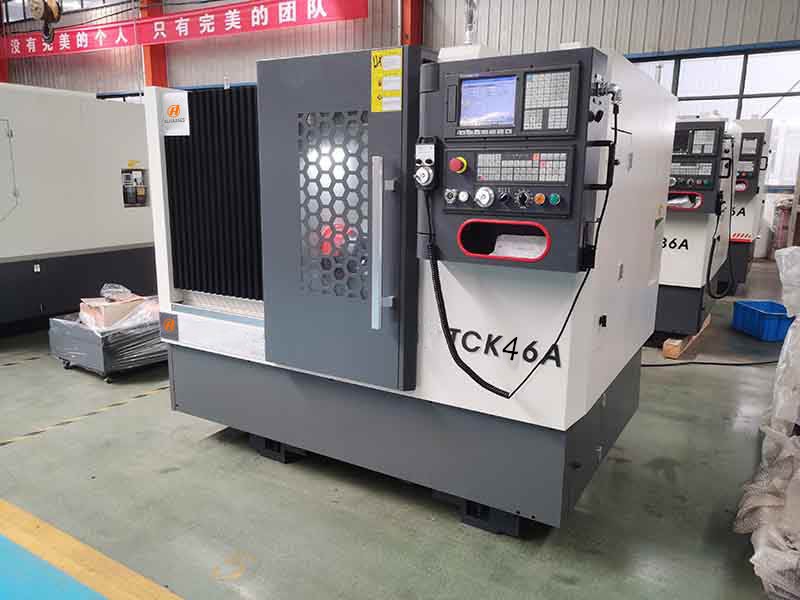
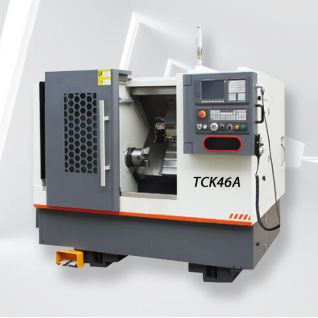
TCK46A Slant Bed CNC Lathe
The TCK46A is a slant bed CNC lathe for small and medium precision parts: Φ460 mm swing over the bed, Φ260 mm over the slide, 350 mm machining length and a 3500 rpm spindle with a Φ56 mm bore. CE certified, with installation and overseas after-sales support.
TCK46A Slant Bed CNC Lathe
The TCK46A is a slant bed CNC lathe built for small and medium precision parts produced in quantity. It pairs a Φ460 mm swing over the bed with a 3500 rpm spindle, a Φ56 mm bore and 350 mm of machining length on a 3000 kg cast structure — a machine sized for valve bodies, fittings, bushings, shafts and connector parts rather than for long shaft work.
The machine is CE certified, supplied with a full manual set, and backed by our overseas after-sales service network. Spare parts and technical support remain available for the working life of the machine.
Key Features
- Φ460 mm swing over bed — the clearance limit, i.e. the largest blank that will rotate over the bed.
- Φ260 mm swing over slide — the working limit once the tool is on the slide. See the note below.
- 3500 rpm spindle — enough speed to run small diameters at correct cutting speed instead of roughing them.
- Φ56 mm spindle bore — bar stock up to Φ56 mm feeds through the spindle for continuous bar work.
- 350 mm machining length — matched to short and medium parts, keeping the structure compact and stiff.
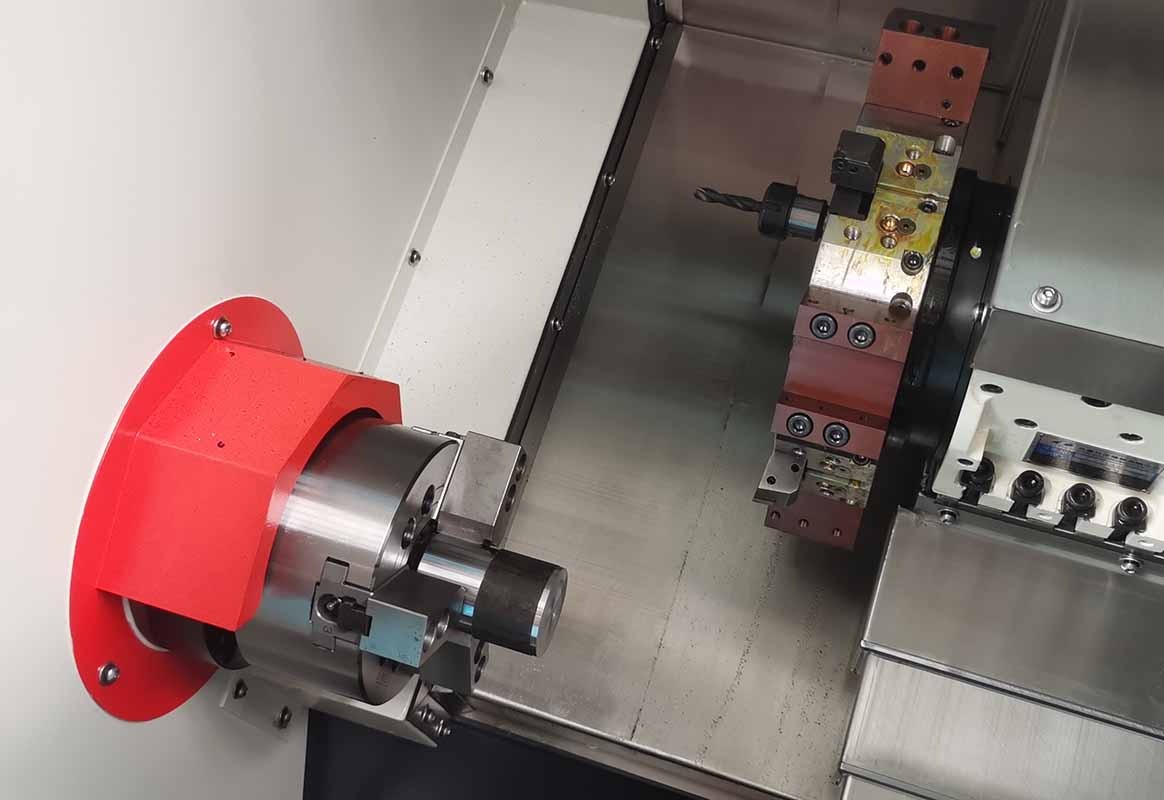
- Slant bed structure — chips fall away from the guideways instead of packing into them.
- 3000 kg machine weight — real mass behind the spindle, so finish does not depend on light cuts.
Φ460 Over the Bed, Φ260 Over the Slide — Read Both Numbers
These two figures are not interchangeable, and quoting only the larger one is how a machine gets bought for work it cannot do. The Φ460 mm swing over bed is a clearance figure: it tells you the largest blank that will physically rotate over the bed without fouling. The Φ260 mm swing over the slide is the working figure: once the tool is mounted on the slide, this is the diameter range you can actually turn.
For the TCK46A, plan your process against Φ260 mm. The Φ460 mm figure is what lets you chuck awkward or off-centre blanks without a riser block — useful, but not a machining capacity.
Why a Slant Bed Matters in Production
On a flat bed lathe, chips land on the guideways and stay there. On a part running at 3500 rpm in a production cycle, that means abrasive swarf being dragged across a precision surface several hundred times per shift. A slant bed lets chips fall clear into the chip pan, which keeps the guideways clean and holds accuracy over months instead of weeks.
The slant layout also puts the spindle and turret closer to the operator, which shortens setup and tool change time. On short cycle parts, that time is a larger share of total cost per piece than the cutting itself.
3500 rpm for Small and Medium Diameter Finishing
Cutting speed is diameter times rpm. At 3500 rpm, a Φ25 mm part runs at roughly 275 m/min — a normal finishing speed for steel with carbide. On a lathe limited to 1500 rpm, the same part runs at under 120 m/min, which is a roughing speed: the finish suffers and the insert wears faster than it should.
This is the practical reason the TCK46A is specified with a 3500 rpm spindle. High spindle speed is not a headline number here; it is what lets a Φ10–Φ80 mm part reach the surface finish the drawing asks for without a second operation.
Φ56 mm Bore for Bar Work
A Φ56 mm spindle bore puts the TCK46A into continuous bar work: stock feeds through the spindle, the part is cut off, and the cycle repeats without an operator opening the chuck. For turned parts produced in hundreds or thousands, that removes the loading time from every single piece.
Bar work also holds length consistency better than repeat chucking, because the part is always referenced to the same stop position rather than to how carefully the operator seated it.
350 mm of Machining Length — Where This Machine Fits
350 mm is short by design. A bed long enough for occasional long parts is longer, heavier and more expensive for every part it makes, including the short ones. If your work is mostly under 350 mm, a short-bed machine holds tolerance better because there is less structure to deflect and less bed to thermally grow.
If your parts are regularly longer than 350 mm, this is the wrong model — a longer bed on the same platform is the correct answer, and we will say so rather than sell you into a machine that will not hold your parts.
Applications and Typical Parts
The TCK46A is used wherever small and medium turned parts are made in quantity:
- Hydraulics and pneumatics — valve bodies, spools, fittings, union nuts
- Automotive — sensor housings, bushings, shafts, fastener blanks
- Electronics and instruments — connector shells, terminals, instrument spindles
- General engineering — pins, sleeves, spacers, threaded adaptors
It machines carbon steel, alloy steel, stainless steel, brass, aluminium and engineering plastics with the appropriate inserts and cutting parameters.
CNC System and Configuration Options
The machine is supplied with a production CNC system and is configured against your process. Options typically specified with this model include:
- Chuck type and size, including collet chucks for bar work
- Bar feeder interface matched to your stock diameter and length
- Turret arrangement, driven tooling where the process needs it
- Parts catcher and chip conveyor for unattended short cycles
- Coolant and air blast arrangement for the materials you run
Configuration drives both cycle time and price, so the final specification is confirmed against your drawing before quoting.
Installation, Commissioning and Support
At 3000 kg with overall dimensions of 2500 × 1700 × 1890 mm, the TCK46A ships as a complete machine and does not need a special foundation in a normal workshop. We supply foundation drawings, the electrical schematic and the parameter list before the machine leaves the factory.
Commissioning covers levelling, spindle warm-up and runout check, tool setting and a first-part run. Training for your operators and maintenance staff is included, and our overseas after-sales service network keeps spare parts and technical support available for the working life of the machine.
Technical Specifications
| Item | Unit | TCK46A |
| Max. swing diameter over bed | mm | Φ460 |
| Max. swing diameter over slide | mm | Φ260 |
| Max. machining length | mm | 350 |
| Spindle speed | rpm | 3500 |
| Spindle bore diameter | mm | Φ56 |
| Machine weight | kg | 3000 |
| Overall dimensions (L×W×H) | mm | 2500 × 1700 × 1890 |
All figures above are for this model as supplied. Note once more that Φ460 mm is swing over the bed (clearance) while Φ260 mm is swing over the slide (working limit). Confirm the final data sheet with us before ordering.
Why Choose TCK46A
- CE certified — documentation supplied for EU import and site acceptance.
- Overseas after-sales service — engineers and spare parts support in Europe.
- 3500 rpm spindle — small and medium parts finished at correct cutting speed.
- Slant bed — chips clear the guideways, so accuracy is held over months of production.
- Φ56 mm bore — continuous bar work without opening the chuck between parts.
- 3000 kg of structure — mass behind the spindle, not a light frame at high rpm.
Send us a drawing and the monthly quantity. We will confirm whether the TCK46A suits the part, quote the configuration, and tell you plainly if another model fits better.